Über uns
Ihr Experte Hersteller von Wedge Wire Screens;
Ihr zuverlässiger Partner und Innovationsquelle
Erhalten Sie ein kostenloses Angebot
-
Startseite

-
Blog
-
Branchenblog
- Heavy-Media Recovery With Wedge Wire Vibrating Screens
Heavy-Media Recovery With Wedge Wire Vibrating Screens
-
 Autor
- 14,Oktober
A drain-and-rinse screen is a small part of a dense-medium circuit, but it can decide how much magnetite or ferrosilicon returns to the loop with usable density. The screen has to shed liquid promptly while moving solids predictably, even when the feed is abrasive, wet, and uneven. That is why screen media deserves attention as an operating surface, not merely as a replaceable panel.
What a drain-and-rinse deck has to do
Heavy-media recovery begins by separating valuable dense medium from the sized mineral stream so it can be cleaned, reconditioned, and reused. On a vibrating screen deck, the drain portion removes the bulk of the medium that travels with the solids. The rinse portion then displaces residual medium with water, helping keep the product stream and the returned medium circuit from contaminating one another.
Drain and rinse are separate jobs
The drain zone needs fast liquid passage without losing the particle fraction that the process intends to retain. The rinse zone needs a stable bed so wash water can contact entrained medium instead of simply short-circuiting through bare patches. When those duties blur together, extra water often masks the real issue: uneven feed spread, a poor deck angle, or media that no longer drains at the expected rate.
Why the sieve screen surface changes the result
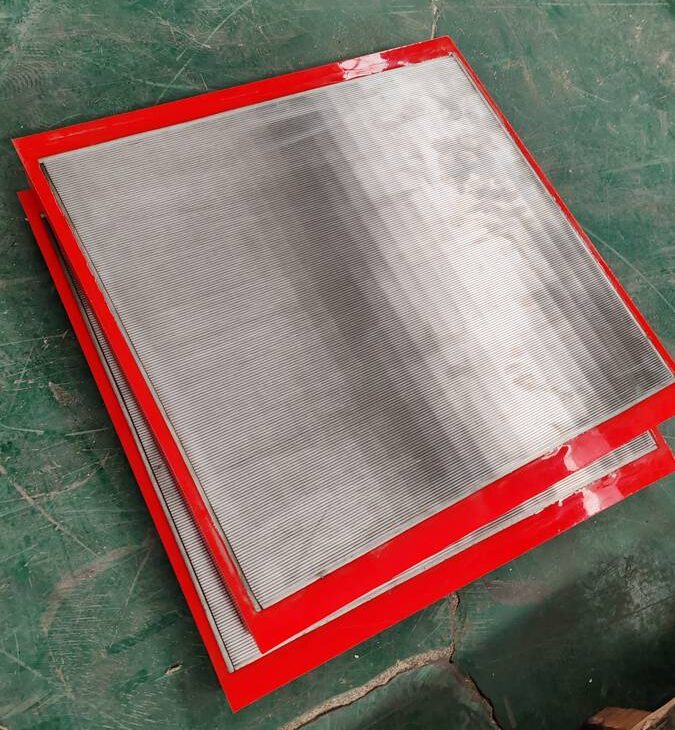
A stainless steel vibrating screen mesh must keep its opening geometry under vibration and slurry abrasion. BTOSLOT lists 304, 316L, and 321 stainless steel, with 0.1–5 mm slots and 25–45% open area. Those values are a starting point, not a universal setting for every circuit.
The V-profile releases liquid while reducing deep particle lodging. In heavy-media service, the benefit still depends on profile wire, support spacing, slot direction, and frame stiffness matching the motion and feed. A screen can drain poorly when material piles up in one lane or fines coat the screen surface.
Open area is useful only when the Keildrahtsieb bed stays controlled
The phrase offene Fläche des Keildrahtsiebs is not a shortcut for throughput. It is one part of a balance among drainage, retention, support, and wear life. More flow path can help drainage, yet a sieve screen with poor support or an unstable bed creates a different recovery problem.
Open area has a trade-off
Plant teams should compare clean-water drainage, operating drainage, retained-medium loss, and wire condition at the same duty. This makes panel choice testable: does the sieve screen move solids and liquid as the circuit needs?
| Operating signal | What it can mean | Useful response |
| Medium appears in the solids discharge | Slot is too open for the actual particle size, or the bed is too thin to present particles to the deck. | Check particle-size distribution, bed depth, and slot choice before changing the screen motion. |
| Drain water remains visibly dense | The sieve screen is draining slowly, often because the effective open area is reduced by wear, blinding, or a poor feed spread. | Inspect the feed box and screen surface; compare clean and operating drainage rather than judging by nominal aperture alone. |
| Wash stage consumes more water but recovery does not improve | The issue may be carryover or uneven material travel, not simply insufficient rinse flow. | Stabilize feed distribution and discharge pattern, then tune the wash-water addition against a measured recovery result. |

The operating details that deserve attention
The screen cannot correct every upstream fluctuation, but it should give operators a repeatable response when feed changes. A rise in clay, fine particles, or slurry density can alter sieve screen behavior before sampling reveals the impact. Inspect feed spread, screen blinding, discharge pattern, and rinse distribution before changing several variables.
For teams comparing slurry screen manufacturer options, focus on material, slot orientation, support-rod layout, panel dimensions, and vibration duty. Those details match the surface to the machine and mineral stream better than a generic non-blinding claim.
The same discipline applies to a Johnson screen filter element for mineral processing filtration. It should be discussed in the context of a specific duty, not as a catch-all answer for every slurry. Heavy-media recovery needs a robust vibrating screen; other points may need another geometry screen.
- Feed spread across the full deck width.
- Bed depth and any visible blinding during the shift.
- Medium loss measured with the same sampling method each time.
A practical reading of performance changes
Performance changes are easier to diagnose when the circuit has a baseline. Record medium density before and after the screen, retained-medium losses, rinse-water rate, feed distribution, and how the panel looks after a defined operating interval. When results move together, the operating team can distinguish a media-quality issue from a drainage or deck-surface issue.
The term vibrating wire screens covers many layouts, so replacement decisions should not be made from aperture alone. A compatible replacement must fit the screen frame and preserve the intended flow direction, support pattern, and panel restraint. In an abrasive service, wear should be checked for its effect on cut behavior as well as for visible breakage.
Summary: recovery depends on a stable separation surface
A wedge wire vibrating deck can support heavy-media recovery when it drains promptly, retains the intended solids, and remains stable under the actual feed and vibration duty. The sensible next step is to measure where medium is leaving the circuit, inspect how the screen bed behaves across the sieve screen, and define the slot, support, and panel details around that evidence.
Häufig gestellte Fragen
What is the purpose of the rinse stage in heavy-media recovery?
The rinse stage removes dense medium that remains with the solids after the drain section. It helps return medium to the recovery circuit while limiting contamination in the product stream. The right rinse rate depends on bed behavior and recovery measurement, not on a fixed water setting.
Can one wedge wire vibrating screen panel suit every mineral slurry?
No. Particle size, medium type, solids loading, abrasion, vibration motion, and the target separation all affect the suitable panel design. A panel that works well for one drain-and-rinse duty may not be appropriate for a fine dewatering or classification task.
Why can a Bildschirm deck drain slowly even when the slot is not blocked?
Uneven feed distribution, a thick material bed, poor rinse placement, or a change in slurry characteristics can restrict effective drainage. Inspecting the working screen deck is important because a clean, static panel does not fully represent operating flow.
Does a wider slot always improve heavy-medium drainage?
A wider slot can increase liquid passage, but it can also change what reports to the undersize stream. Slot selection needs to protect the process cut while supporting drainage, so it should be evaluated against particle-size data and recovery results.
What should be supplied when specifying a replacement vibrating panel?
Provide the screen model or clear frame dimensions, feed material and particle-size range, medium used, desired separation duty, slot direction, operating hours, and the failure or recovery issue being observed. This gives the screen designer enough context to propose a compatible surface.
Letzter Beitrag
Verwandte Produkte
Bestverkaufte Produkte
Stärke Screen
Der Wedge Wire Starch Curved Screen ist ein gekrümmtes Siebgerät, das speziell für die Stärkeindustrie entwickelt wurde. Es verfügt über eine bogenförmige Siebfläche aus präzise geschweißten V-Profil-Edelstahldrähten, die Zentrifugalkraft oder Schwerkraft nutzen, um eine schnelle Entwässerung und Klassifizierung von Stärkeslurry zu erreichen. Seine gekrümmte Struktur verlängert die Schlammretentionszeit und verbessert die Effizienz der Feststoff-Flüssigkeit-Trennung. Es eignet sich für Stärkeextraktion, Raffinierung und Nebenproduktrückgewinnungsprozesse für Stärke wie Kartoffel, Mais und Cassava. Diese Ausrüstung ist durch eine effiziente Siebung, Verschleiß- und Verstopfungsbeständigkeit und einfache Wartung gekennzeichnet und ist eine Schlüsselvorrichtung zur Feststoff-Flüssigkeit-Trennung in der modernen Stärkeverarbeitung.
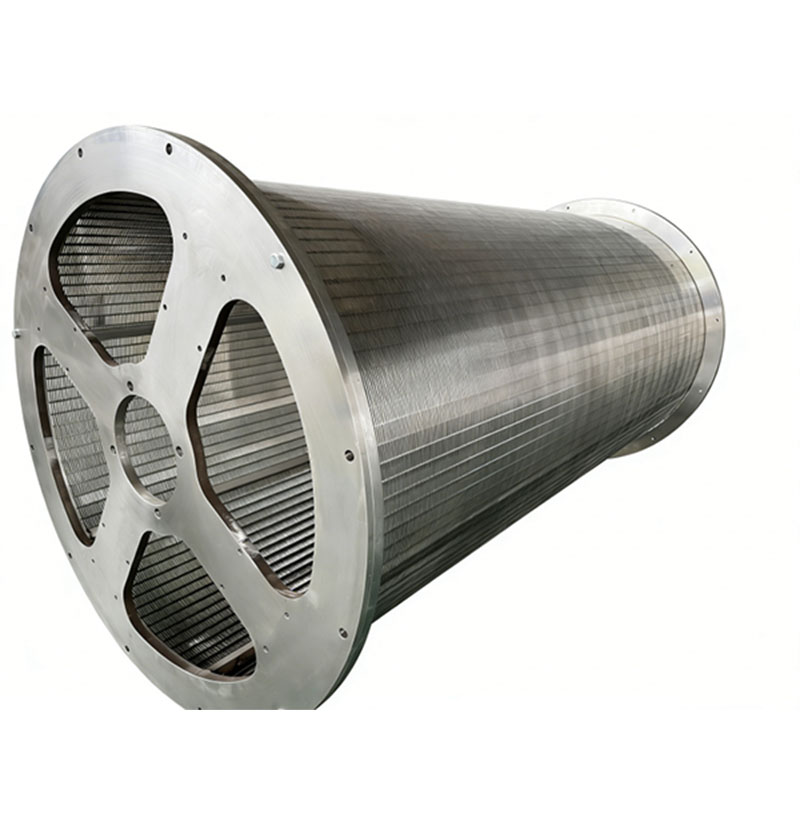
Rotierende Trommel
Der Edelstahl Keil Draht Rotary Drum Screen (auch bekannt als ein Rotary Drum Sieb oder Micro-Screen) ist eine kontinuierlich und automatisch arbeitende Front-End-Feststoff-Flüssigkeit-Trennvorrichtung. Sein Kernbauteil ist eine große zylindrische Trommel, die horizontal oder leicht geneigt installiert ist. Die gesamte Umfangsfläche der Trommel ist mit einem Edelstahlkeildrahtsieb (Johnson-Sieb) bedeckt. Das zu behandelnde Abwasser strömt in ein Ende der Trommel. Unter Schwerkraft passiert das Filtrat durch die Keildrahtschlitze, während feste Suspensionsstoffe (wie Fasern, Haare, Kunststoffstücke und feine Partikel) auf der Innenfläche der Trommel gehalten werden. Während sich die Trommel langsam dreht, wird der zurückgehaltene Trümmer nach oben angehoben, wo er durch Sprühwasser in eine Sammeltage gespült wird, wodurch ein kontinuierlicher Prozess der automatischen Siebung, Filtration und Rückstandsentfernung erreicht wird.
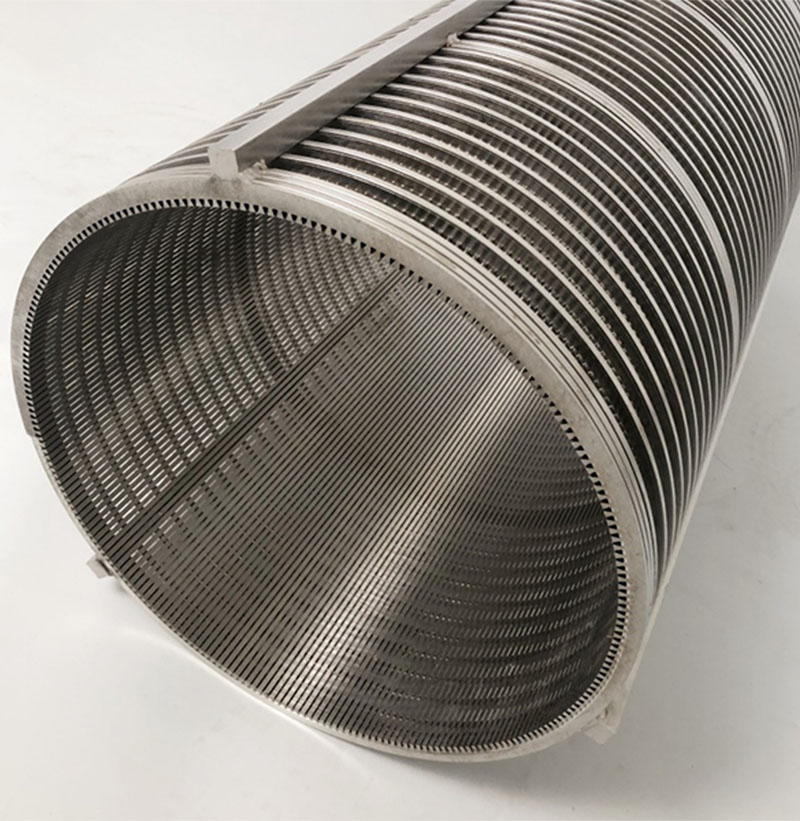
Siebkorb für Screw Press Separator
Der Edelstahl Keil Draht Sieb Korb, allgemein bekannt als der "V-Draht Sieb", "Presse Sieb Korb" oder "Sieb Zylinder", ist ein Kernkomponent der Schraubpresse Fest-Flüssigkeit-Separatoren. Es ist innerhalb der Spiralpresse installiert und umschließt die rotierende Schraubenwelle. Das Arbeitsprinzip lautet wie folgt: Rohslurry mit hohem Feuchtigkeitsgehalt wird durch die Schraubenwelle in den Siebkorb geschoben. Unter der Druck- und Förderwirkung der Spiralflüge wird die Flüssigkeit (Filtrat) durch die präzisen, kontinuierlichen Schlitze des Siebkorbs herausgedrückt, während das feste Material (Düngkuchen) im Inneren gehalten wird und weiterhin komprimiert und entwässert wird, während es sich nach vorne bewegt. Schließlich werden die entwässerten Feststoffe aus dem Auslass abgegeben, wodurch eine Feststoff-Flüssigkeit-Trennung erreicht wird.
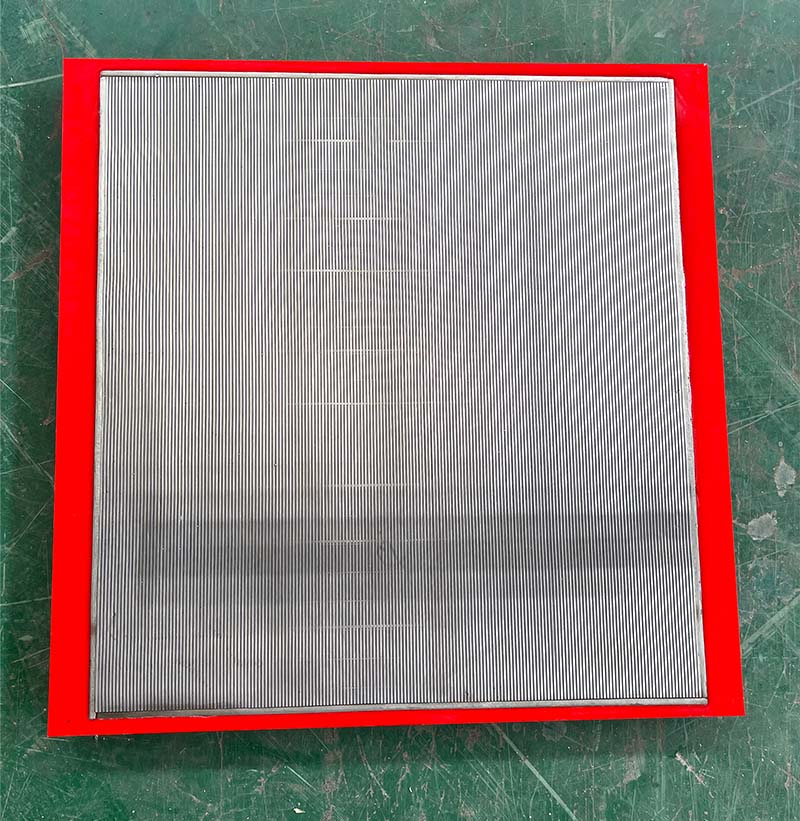
Keil Draht vibrierende Bildschirm
Ein Edelstahlkeildraht-Vibrationsschirm ist eine Fest-Flüssigkeit-Trennvorrichtung mit einer Siebfläche, die durch präzises Schweißen von V-förmigen Edelstahldrähten hergestellt wird, die in ein Hochfrequenzsvibrationssystem integriert ist. Mit einheitlichen Schlitzen, Verschleißbeständigkeit und Korrosionsbeständigkeit ist es für Nasssieb- und Entwässerungsvorgänge geeignet. Der Vibrationsmechanismus ermöglicht eine schnelle Materialverteilung und ein effizientes Sieben, während ein Verstopfen des Siebs effektiv verhindert wird. Weit in Industrien wie Bergbau, Metallurgie, Lebensmittelverarbeitung und Umweltschutz eingesetzt, ist es besonders geeignet für den Umgang mit feinen Partikeln, hochviskosen oder leicht agglomerierenden Materialien und bietet Vorteile wie hohe Siebgenauigkeit, große Verarbeitungskapazität und lange Lebensdauer.
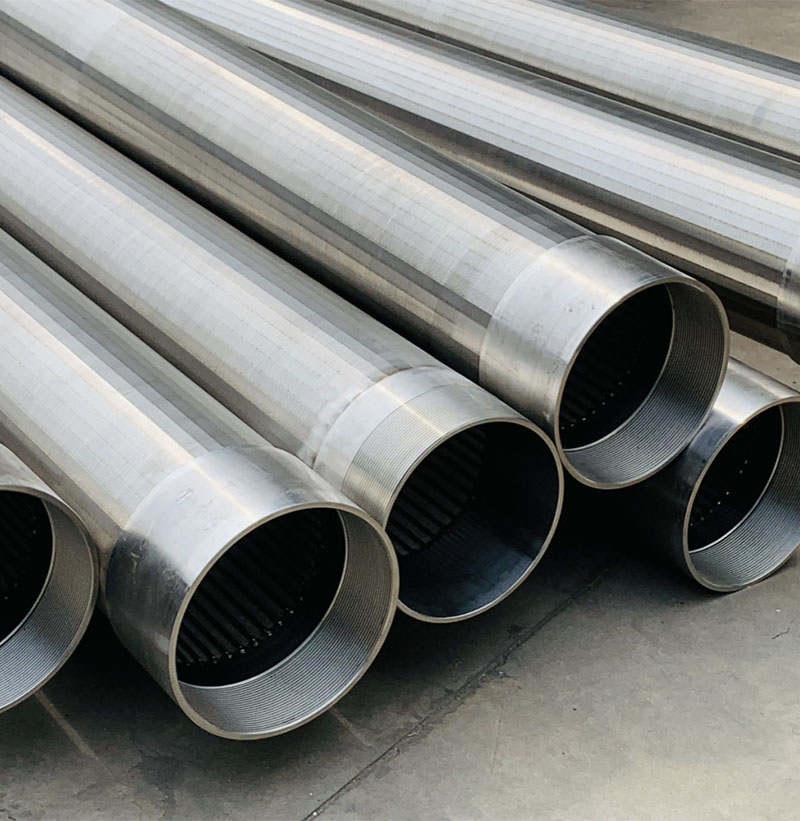
Keil Draht Wasser Brunnen Bildschirm
Johnson Deep Water Well Screens, auch als Continuous Slot Screens oder Wire Wrap Screens bezeichnet, wurden ursprünglich entwickelt, um Herausforderungen bei der Sandkontrolle in feinkörnigen und gleichmäßigen Sandformationen zu lösen. Diese geologischen Bedingungen sind häufig in tiefen Grundwasserwässern zu finden, wo herkömmliche Lochröhren oft unter Verstopfungen, übermäßiger Sandproduktion und reduzierter Brunneneffizienz leiden.
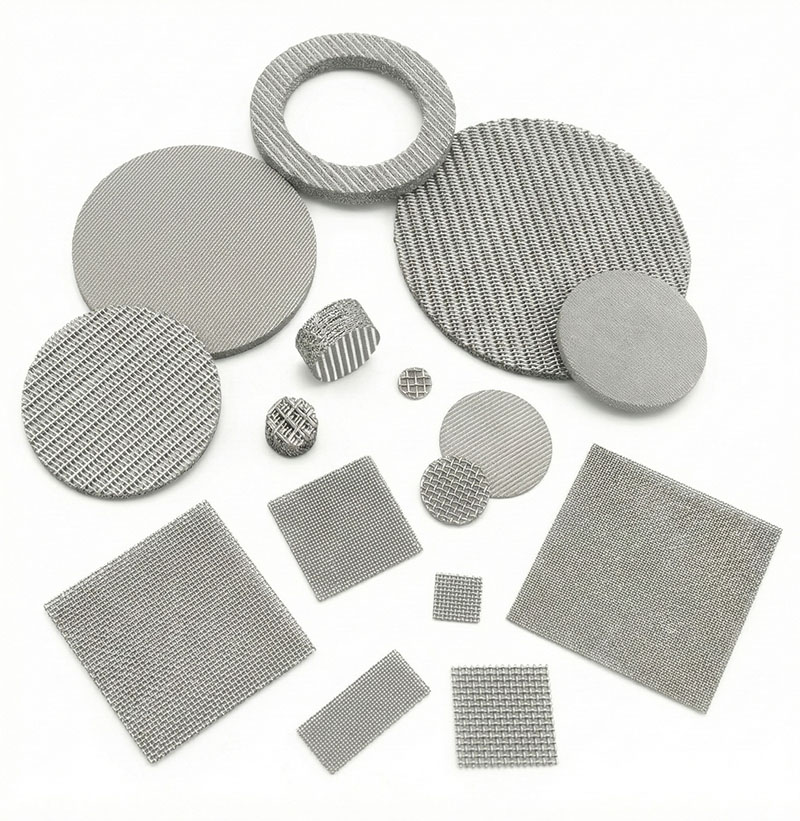
Sinterte Mesh Platte und Scheibe
Sintermaschenplatten und -scheiben sind hochpräzise Filtrationskomponenten, die durch das Verbinden mehrerer Schichten Edelstahldrahtmaschen durch einen spezialisierten Vakuumsinterprozess hergestellt werden. Im Gegensatz zu herkömmlichen Netzen, die sich allein auf mechanisches Weben verlassen, werden diese Platten an jedem Kontaktpunkt geschmolzen und verwandeln einzelne Drähte in ein starres, integriertes poröses Blech.Diese Platten können in verschiedene Formen angepasst werden, am häufigsten kreisförmige Scheiben, um spezifische Industriegeräte anzupassen. Sie bieten eine ideale Balance aus hoher Durchlässigkeit, extremer struktureller Integrität und präzisen Filtrationswerten. Da sie ausschließlich aus Metall (typischerweise 304 oder 316L) hergestellt sind, bieten sie eine "permanente" Filtrationslösung, die hohen Temperaturen und korrosiven Chemikalien standhalten kann, während sie vollständig reinigbar und wiederverwendbar bleiben.